
Yet after examining medical-mask requirements and provider quotes, I have actually learned that a neat basis-weight number can conceal more than it exposes: weak electrostatic charging, inconsistent fiber size, excessive breathing resistance, unpredictable manufacturing great deals, or a filter layer silently substituted after authorization.
So why do order still deal with GSM as the main efficiency need?
Because it is simple to gauge. Filtering performance is harder.
A meltblown layer evaluating 25 grams per square meter may surpass a nominally “better” 30 GSM layer if its polypropylene material, fiber circulation, web uniformity, electret treatment, and thermal history are much better controlled. The unpleasant fact is that purchasers frequently define the easiest attribute to inspect as opposed to the feature people actually rely on.
My position is candid: never ever approve meltblown fabric for clinical mask orders on GSM alone. Set GSM as a regulated construction criterion, then bind it to microbial filtering efficiency, particulate filtration effectiveness, differential pressure, fluid resistance, product identity, and lot-level verification.
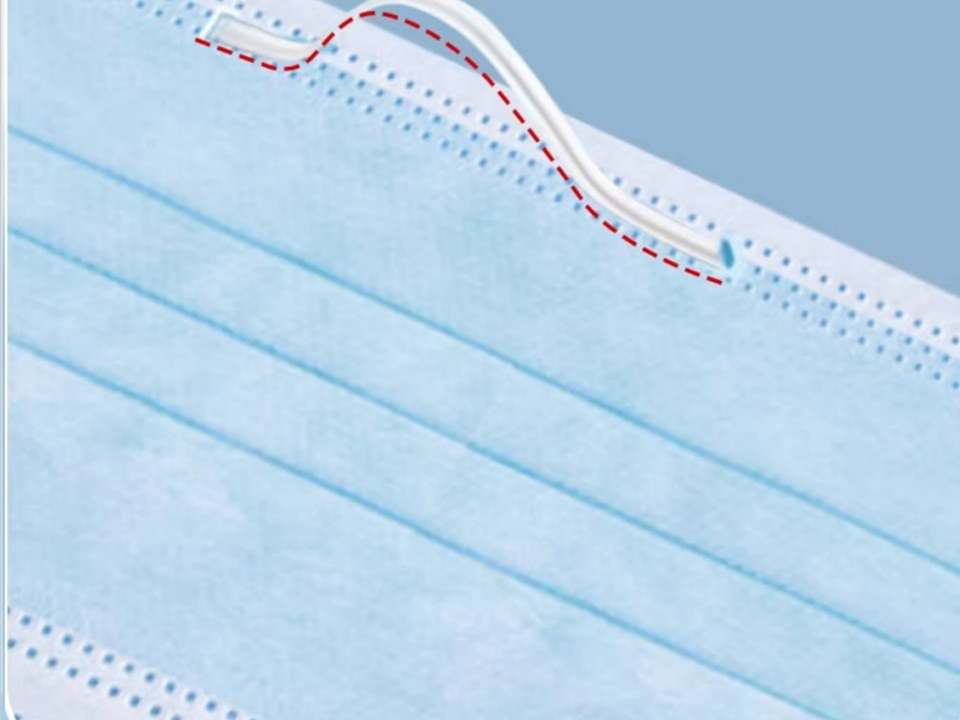
What Does Meltblown Material GSM In Fact Determine?
Meltblown fabric GSM is the basis weight of the nonwoven internet, revealed in grams per square meter, or g/m ². It tells a buyer how much product occupies a specified area, yet it does not straight establish purification performance, breathability, electrostatic cost, fiber diameter, liquid resistance, or regulatory compliance.
That distinction issues.
Two rolls can both be noted 25 GSM while acting really differently. One may have a penalty, evenly dispersed polypropylene fiber web with resilient electret billing. The various other might show slim areas, larger fiber packages, weak cost retention, and undesirable pressure decrease.
The invoice will certainly call them equal. The research laboratory will not.
GSM remains beneficial for three factors:
- It helps control material usage and mask weight.
- It can disclose unapproved building modifications.
- It gives a reproducible incoming-inspection specification.
But GSM is a finger print, not a judgment.
The Hard Fact: More GSM Does Not Immediately Mean Better Filtering
Adding meltblown product can enhance the mechanical capture of bits, but it can additionally increase breathing resistance. That creates a design trade-off: filtering should improve without making the completed mask unnecessarily challenging to take a breath via.
Cost complicates the equation.
Medical-grade meltblown polypropylene, commonly composed as PP and chemically represented by the repeating hydrocarbon unit ((C_3H6) n), commonly obtains corona or hydrocharging treatment. The resulting electret area catches particles without relying completely on a dense physical obstacle.
A well-charged 25 GSM web might for that reason defeat a badly charged 30 GSM internet. And once humidity, heat, solvents, storage space time, or inadequate process control damages that bill, the appealing lab arise from a carefully picked sample might not endure business production.
That is why I question in need of support phrases such as “medical quality,” “high purification,” and “BFE 99%.” Which approach was made use of? At what circulation rate? On material or on the finished mask? The amount of lots were checked?
No approach, no case.
Advised Meltblown GSM Ranges by Mask Construction
The numbers below are procurement starting points, not automatic compliance limits. A buyer ought to change them using verified finished-mask data, the appropriate market criterion, pressure-drop targets, and the vendor’s demonstrated process capability.
| Mask building and construction | Practical starting range for meltblown layer | Common filter arrangement | Purchase position |
|---|---|---|---|
| 3-ply treatment mask | 20– 25 GSM | One meltblown layer | Accept only with finished-mask BFE and differential-pressure information |
| ASTM Level 1 medical mask | 20– 25 GSM | One billed meltblown layer | Support breathability, yet confirm ≥ 95% BFE under the appropriate technique |
| ASTM Level 2 medical mask | 25– 30 GSM | One higher-efficiency layer or crafted composite | Call for ≥ 98% BFE plus fluid-resistance and pressure-drop outcomes |
| ASTM Level 3 clinical mask | 25– 35 GSM | Higher-performance meltblown or multi-web layout | Do not infer Degree 3 condition from GSM; need full test evidence |
| KN95-style respirator | 40– 60 GSM total meltblown is an usual design window | One or more meltblown layers | Review the complete respirator under the declared criterion |
| High-breathability customized mask | Supplier-defined | Low-resistance electret media | Define optimum stress drop and minimum filtration concurrently |
| Industrial dirt mask without certified filtration | None or construction-dependent | Spunbond shell, optional filter | Never market it as a medical mask or qualified respirator |
These varieties are deliberately wide. There is no straightforward global solution to “What is the most effective GSM for meltblown fabric?” without knowing the needed test method, mask geometry, variety of filter layers, target air movement resistance, and designated regulatory category.
As an example, a standard 1-ply PP spunbond mug dust mask for bulk sourcing belongs to a different item category from a clinical mask consisting of a verified meltblown filter. Similar look does not create similar efficiency.
Clinical Mask, Dirt Mask, and KN95 Specifications Are Not Interchangeable
This is where procurement teams get harmed.
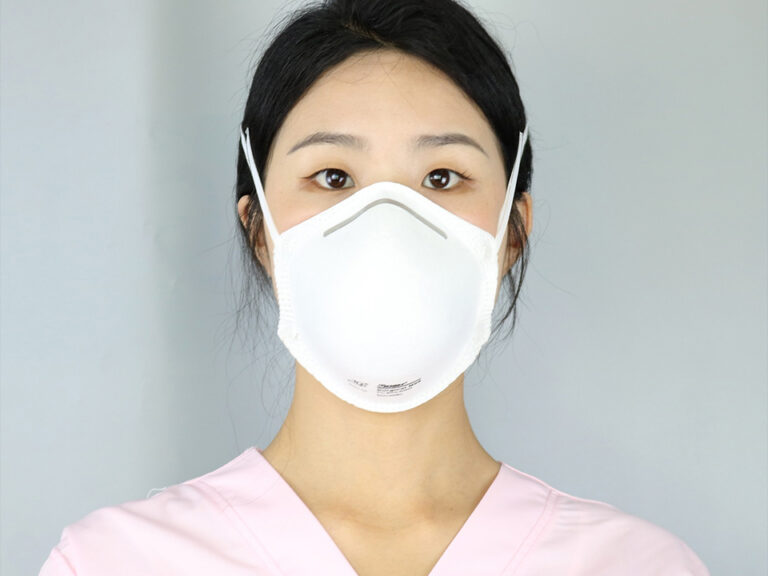
A loose-fitting medical mask is typically evaluated for source control, microbial filtration, sprinkle resistance, breathability, and various other demands under the appropriate medical-mask structure. A filtering facepiece respirator is made to secure against the face and is assessed as a complete respiratory-protection device.
A cup form verifies nothing. 5 layers show nothing. Also the existence of meltblown material shows little bit unless the completed product meets its asserted criterion.
The FDA’s August 26, 2024 recap for PRIMED versions K240286 described clinical masks containing a meltblown polypropylene filter in between nonwoven layers and analyzed Level 1 and Level 3 products under ASTM F2100-2023. The filing additionally made a vital point that sales brochures typically blur: adjustments in layer basis weight and building and construction must be supported by finished-device testing, not assumption. See the FDA 510(k) recap for K240286.
For respirator procurement, a 5-ply flat-fold KN95 earloop design might be the right commercial beginning factor, but the order still needs the asserted requirement, model-specific report, test research laboratory, example identification, production-lot controls, and packaging traceability written right into the contract.
The item name is advertising and marketing. The examination document is proof.
Build the Purchase Spec Around Efficiency, Not Material Weight
I would certainly create the material spec in five layers.
First, determine the polymer. Call for virgin polypropylene ideal for the verified manufacturing procedure unless recycled web content has actually been specifically evaluated and authorized. State allowed ingredients, colorants, and processing aids.
Second, define construction. Define the small meltblown fabric GSM, resistance, variety of layers, usable width, roll size, winding requirements, splice restrictions, and alignment.
Third, define filtering. Call the specific test technique, aerosol or organism, particle size or circulation, conditioning procedure, face velocity or flow price, minimal outcome, and number of samplings.
4th, control breathability. Establish maximum differential stress under the method applicable to the ended up mask. A provider ought to not be allowed to rescue purification by merely generating a denser, less breathable web.
Fifth, lock the approved style. Resin grade, melt-flow rate, electret procedure, layer matter, basis weight, equipment line, and subcontractor must not change without composed approval and revalidation.
A convenient purchase-order condition could read:
The medical mask filter layer will include electret-treated meltblown polypropylene at 25 GSM nominal, controlled within the buyer-approved resistance. Compliance needs sufficient finished-mask filtering, differential-pressure, fluid-resistance, flammability, and biocompatibility proof under the criteria specified in this requirements. GSM consistency alone does not make up acceptance.
For a commercial order developed around a 5-ply KN95 earloop respirator, I would include a model-specific consistency record and a restriction on unauthorized modifications to nose cord, straps, welding parameters, filter layers, or facepiece dimensions. Those parts influence leakage and fit also when the filter media itself performs well.
Convert “25 GSM” Into an Enforceable Tolerance
A small worth without a tolerance is incomplete work.
Do not create only “25 GSM meltblown.” State the allowed variety and the assessment approach. The acceptable tolerance must be based on the accepted manufacturer’s process ability and item recognition, not duplicated thoughtlessly from a contending quotation.
As an example:
- Nominal basis weight: 25.0 g/m ² Commercial resistance: buyer-approved array, such as ± 5%, if validation sustains it
- Examination method: defined sample location, calibrated balance, and conditioning treatment
- Sampling: specimens taken throughout the roll width and along its length
- Reporting: suggest, minimum, optimum, common discrepancy, roll number, and great deal number
- Being rejected guideline: any type of out-of-range unit or whole lot took care of according to the agreed sampling strategy
- Change control: no basis-weight adjustment outside the verified layout window
Why sample throughout the web?
Meltblown lines can create edge-to-center variation. A vendor that cuts every quality-control specimen from the best-performing central area is not demonstrating roll uniformity; it is curating evidence.
I favor a mapped roll account. It is more challenging to adjust and far more useful when a converting line starts generating masks with inconsistent pressure decline.
Demand These Test Outcomes Prior To Authorizing a Vendor
A vendor qualification bundle ought to contain more than a certification carrying a logo design.
Request:
- Finished-mask BFE data under the specified technique
- Finished-mask submicron particulate-filtration information where suitable
- Differential-pressure or breathing-resistance outcomes
- Synthetic-blood infiltration results for the claimed medical-mask degree
- Flammability evidence
- Biocompatibility evidence for skin-contact materials
- Meltblown basis-weight circulation
- Product structure and resin recognition
- Charge-retention or aged-filtration proof
- Three-lot production information rather than a solitary advancement sample
- Lab accreditation extent
- Raw information, specimen matter, conditioning details, and version pictures
- Whole lot coding and traceability records
The FDA’s April 18, 2024 K240258 recap illustrates why the specific typical version and method belong in the data: the assessed item and its predicate used different particulate-filtration strategies, so the company’s comparison depended upon method-specific results rather than a separated performance percentage. That difference appears in the FDA clearance recap for Makrite K240258.
And for N95 cases, NIOSH’s March 2023 assistance informed buyers to validate required markings and approval numbers since fake and misstated respirators stay a genuine procurement danger. The useful lesson is more comprehensive than one certification system: validate the version in the responsible authority’s data source, not in a supplier-created PDF.
If the order concerns a straightforward PP spunbond cup dust mask for wholesale purchase, define it honestly as a dust-mask item unless independent proof supports a more powerful classification. Relabeling a light-weight spunbond shell as a “clinical respirator” is not optimization. It is misrepresentation.
The Supplier Audit Questions That Expose Weak Meltblown Controls
Ask functional concerns. General inquiries welcome brightened solutions.
“What purification performance can you offer?” is weak.
“Program me the last 3 manufacturing whole lots, consisting of basis-weight maps, differential-pressure distribution, electret setups, resin batch numbers, line rate, pass away temperature level, sample conditioning, failings, and restorative actions” is a lot tougher to escape.
I would certainly also ask:
- Which company actually produces the meltblown web?
- Is the converting factory utilizing its very own media or purchasing from a 3rd party?
- What PP material quality and melt-flow rate are approved?
- How is electret charge applied and kept track of?
- How does the factory protect against roll substitution?
- What takes place when GSM passes however purification fails?
- What accelerated-aging proof sustains the shelf-life insurance claim?
- Can every finished-mask carton be mapped to a meltblown roll?
- Which adjustments need buyer notification?
- Are reports tied to the specific version, layer construction, and manufacturing facility on the order?
After that evaluate the records in reverse: carton to manufacturing whole lot, production whole lot to roll, roll to meltblown set, and meltblown batch to resin and electret procedure.
Traceability is tiring. Till it saves an order.
Usual GSM Requirements Failures
The initial failure is defining a solitary number without tolerance. “25 GSM” can come to be 22 GSM in production while the vendor suggests that regular variant was comprehended.
The 2nd is examining basic material yet approving the completed mask by analogy. Ultrasonic welding, pleating, storage space, handling, and building can alter real-world efficiency.
The 3rd is puzzling BFE with respirator filtering. Bacterial filtering performance and respirator particle-filtration examinations use different challenges, methods, and tool assumptions.
The 4th is ignoring differential pressure. A mask that achieves impressive filtration by coming to be intolerably immune to airflow is not a successful style.
The 5th is accepting a report without sampling identity. If the report does not have model photographs, lot numbers, building information, days, and manufacturer identity, it may not explain the goods being delivered.
The 6th is thinking layer count. A white 3-ply mug dust mask with a shutoff need to be judged by its documented intended usage and verified performance, not by the reassuring math of “3 layers.”
Regularly Asked Questions
What is the very best GSM for meltblown fabric in a medical mask?
The best meltblown material GSM is the lowest validated basis weight that constantly satisfies the completed mask’s required purification, differential-pressure, fluid-resistance, and regulatory targets across business manufacturing great deals. For several 3-ply clinical masks, 20– 30 GSM is a sensible development array, but no solitary GSM guarantees ASTM Degree 1, 2, or 3 performance.
A customer must for that reason begin with the target criterion and work backwards. If 25 GSM satisfies the efficiency restricts with ample process margin, transferring to 30 GSM might include expense and breathing resistance without developing a significant benefit.
Is 25 GSM meltblown material ideal for surgical masks?
A 25 GSM meltblown layer is a common design beginning point for surgical-mask advancement, however suitability exists only when the total finished mask passes the relevant purification, differential-pressure, synthetic-blood, flammability, and biocompatibility needs. The very same small textile weight can create different outcomes when fiber framework, charge, building, or production conditions alter.
I would accept a 25 GSM design only after reviewing multi-lot finished-mask information. A textile certificate by itself is insufficient.
Does higher meltblown GSM enhance purification efficiency?
Greater meltblown GSM implies that more fiber mass inhabits each square meter, which may raise mechanical bit capture however can also boost stress decrease and breathing resistance. Filtering also relies on fiber diameter, web uniformity, pore circulation, polypropylene resin, electret charge, layer arrangement, test conditions, and the completed mask’s construction.
So the relationship is not straight. A technically stronger filter is one that gets to the called for purification with controlled resistance and secure production efficiency– not simply the heaviest web offered.
Just how should customers check meltblown material GSM?
Meltblown material GSM should be evaluated by conditioning the material, cutting specimens of a specified area from multiple settings across and along the roll, weighing them with an adjusted equilibrium, and transforming each result to grams per square meter. The tasting strategy must report individual results, standards, diffusion, roll identity, and manufacturing great deal.
Do not accept a single center-cut sampling as proof of roll conformity. Edge-to-center and lengthwise variant can reveal die, airflow, collection, or winding problems that a hassle-free sample misses out on.
Is meltblown GSM sufficient to define a clinical mask filter layer?
Meltblown GSM is not enough to specify a medical mask filter layer since basis weight measures material mass rather than finished-mask security. A defensible spec should also define polymer make-up, electret therapy, layer count, purification methods, differential stress, liquid resistance, flammability, biocompatibility, dimensional controls, great deal sampling, traceability, and change-notification needs.
That solution may irritate purchasers searching for one number. It should. Medical-mask procurement is a performance-control exercise, not a fabric-by-weight purchase.
Should KN95 and medical masks make use of the same meltblown GSM?
KN95 respirators and surgical masks need to not be designated the exact same meltblown GSM by default since they have different buildings, meant uses, examination structures, purification difficulties, airflow problems, and healthy expectations. Their filter systems have to be engineered and checked as full items under the conventional asserted for every precise model.
A provider might use comparable polypropylene meltblown innovation in both items, however that does not make their specifications compatible. Fit and internal leak issue significantly in respirator efficiency.
Transform Your Following Mask Order Into a Controlled Spec
Prior to requesting the following quotation, determine what you are in fact getting: a light-weight dirt mask, a medical face mask, or a filtering facepiece respirator. Then define the standard, finished-product performance, meltblown building and construction, permitted GSM array, test methods, tasting plan, traceability, and change-control regulations.
Do not ask a provider just, “What GSM do you recommend?”
Ask what efficiency the suggested building and construction achieves throughout three manufacturing great deals– and demand the records that confirm it.
Send your desired mask type, target market, yearly volume, required criterion, and recommended construction to the sourcing group for a model-specific quotation and technical testimonial.